Corrosion Is the Design CaseAcid, Caustic, Solvent & Hydrocarbon Duty
Rehman Engineering Works builds and rebuilds the rotating and flow-control equipment that Pakistan's refineries, chlor-alkali, PVC, PTA, soda ash, fertilizer and acid plants depend on — process pumps, valves, alloy castings and reverse-engineered spares, poured, machined and tested at our own Lahore works since 1948.
Pakistan's Chemical Base Runs on Imported Plant and Local Spares
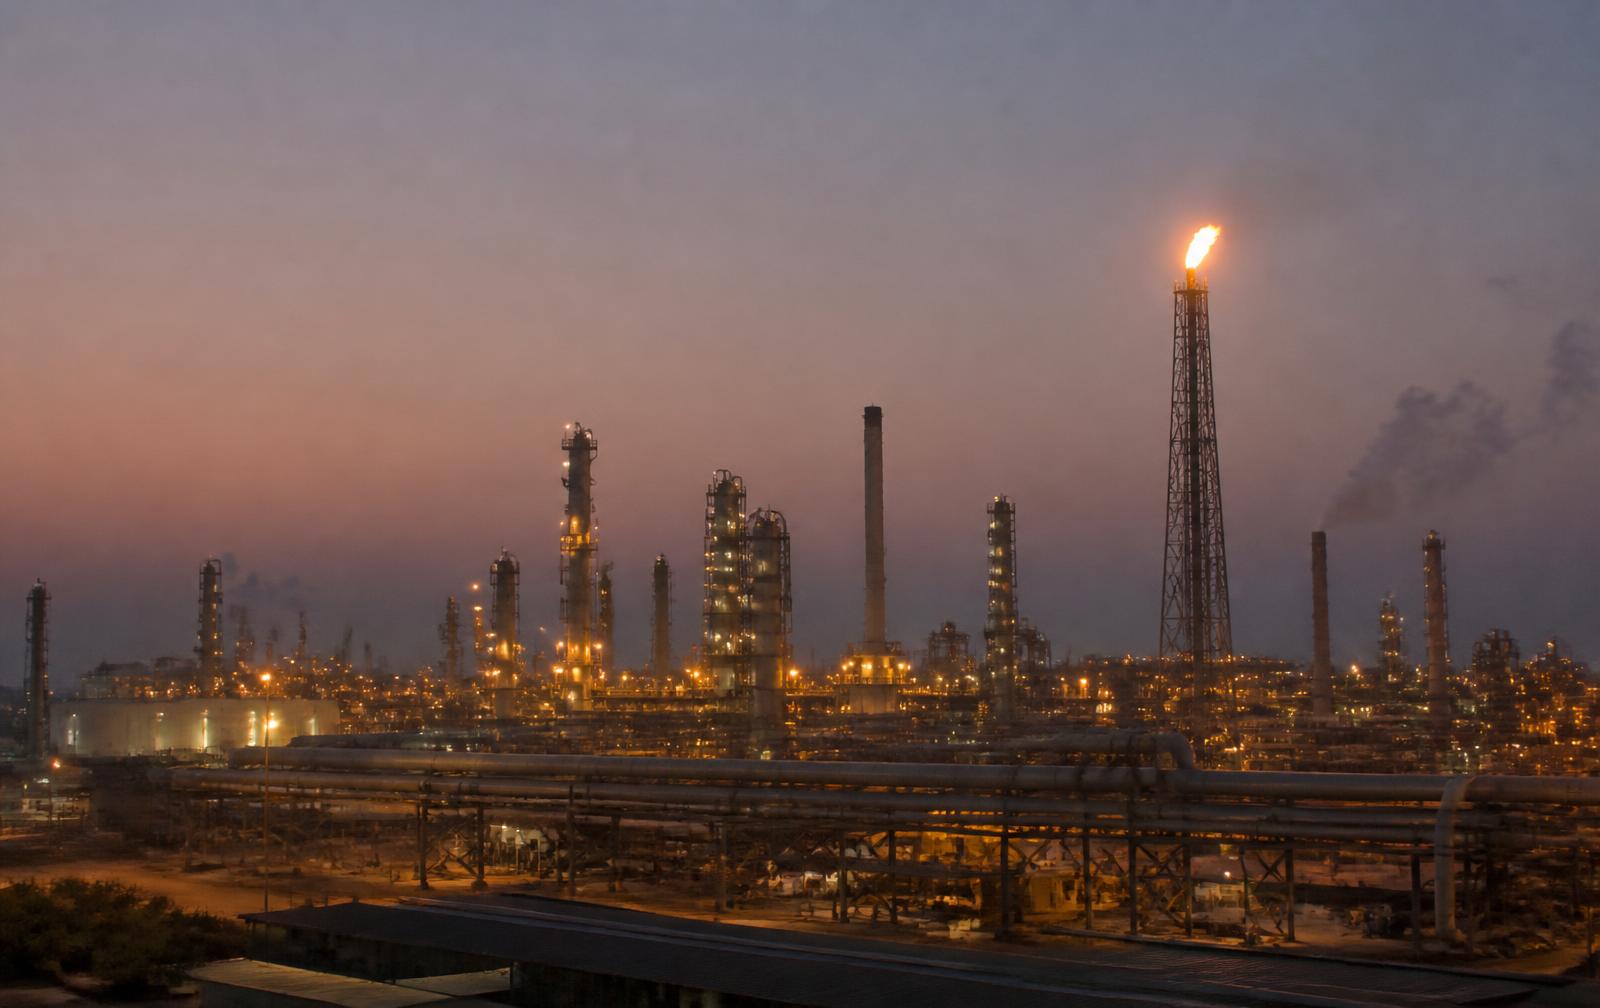
Pakistan's chemical and petrochemical sector is anchored by five operating refineries — PARCO at Mahmood Kot, Pak-Arab and National Refinery and Pakistan Refinery in Karachi, Attock Refinery at Rawalpindi and Cnergyico at Hub — with a combined crude processing capability of roughly 19–20 million tonnes a year. Downstream sit the country's core petrochemical units: PVC and caustic-chlorine at Port Qasim, PTA for the polyester chain, soda ash at Khewra, and a fertilizer complex of ammonia and urea plants at Daharki, Sadiqabad, Mirpur Mathelo, Goth Machhi and Bin Qasim.
Around them is a dense second tier that most equipment vendors ignore: chlor-alkali and bleaching plants in Faisalabad and Kala Shah Kaku, sulphuric and phosphoric acid units, paints, resins, adhesives and industrial gases, agrochemical and pharmaceutical formulation at Hattar, Nooriabad, SITE and Sundar, textile processing chemicals, and tanneries at Kasur and Sialkot. Together these plants consume tens of thousands of pumps and valves — nearly all of them originally imported, most of them now out of support.
That is REW's position in this industry. When the OEM quotes six months and a foreign-currency invoice for an impeller, a valve disc or a casing, we survey the part, select metallurgy against the actual medium, pour it in our own foundry, machine it in Lahore and hand it back with certificates — in weeks, in rupees, to the same or better material specification.
Feedstock to Finished Chemical
Nine unit areas, each with its own corrosion and wear mechanism. Drag the row sideways — every card shows what REW supplies into that stage.
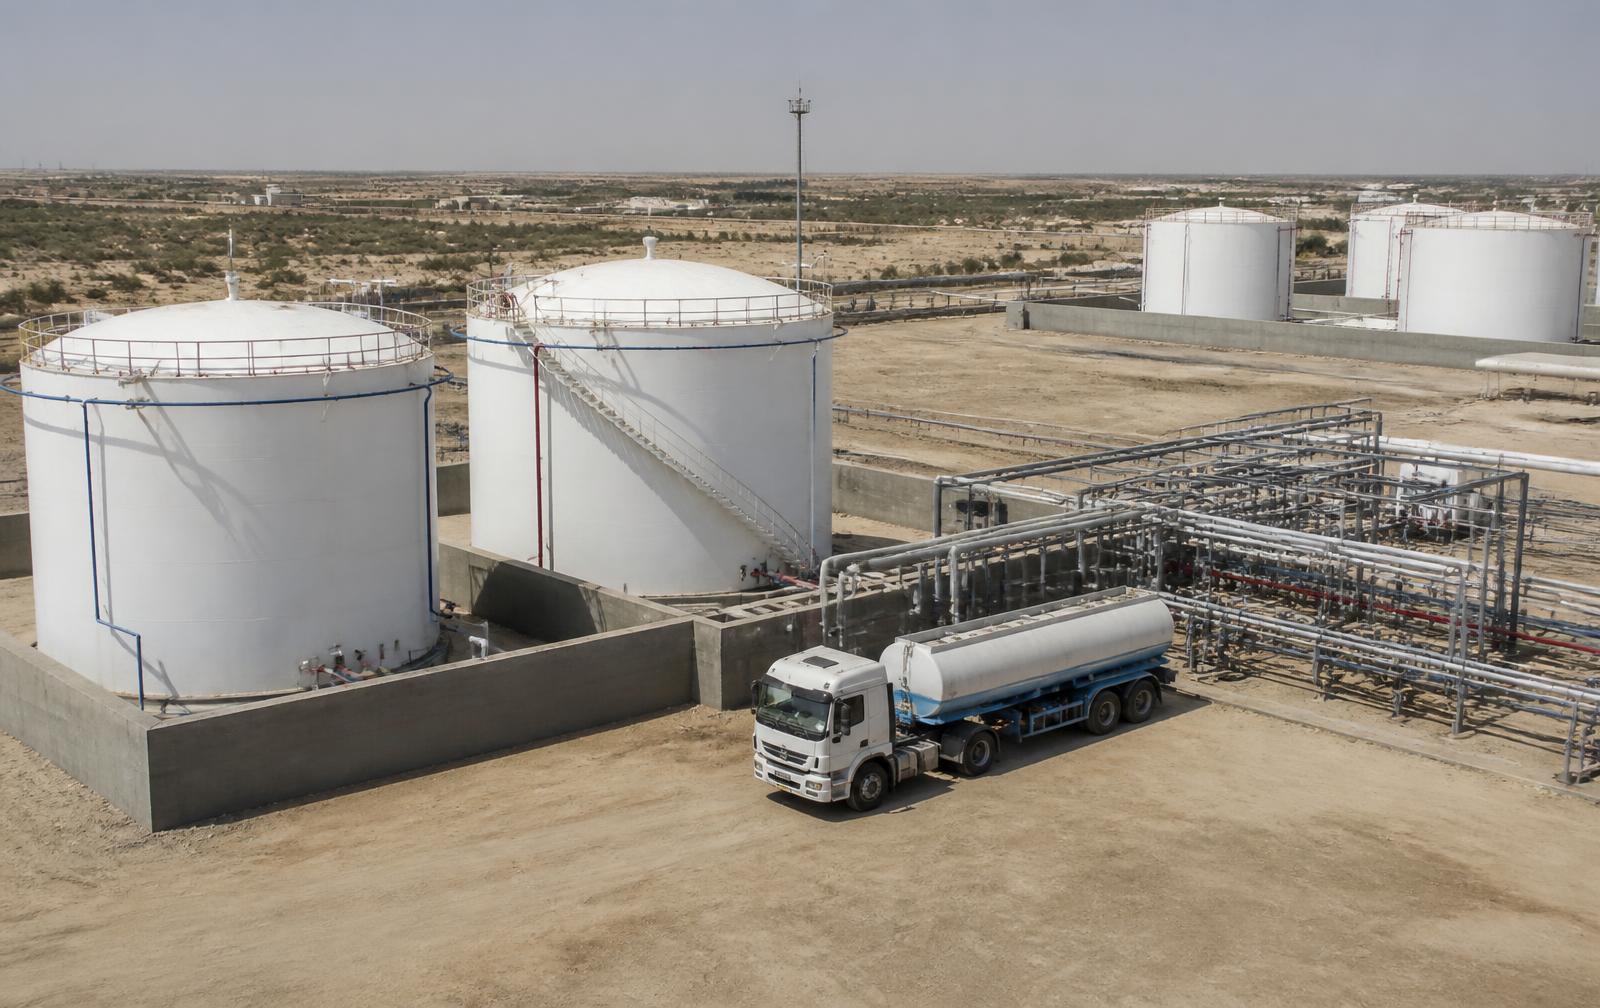
Feedstock Receipt & Tank Farm
Crude, naphtha, brine, sulphur, solvents and acids arrive by pipeline, rail or tanker into bunded storage. Water bottoms, chlorides and tank sludge start the corrosion clock here.
Distillation & Fractionation
Atmospheric and vacuum columns split the feed by boiling range. Overhead lines see wet H₂S and HCl; bottoms see high-temperature naphthenic attack.
Reaction & Conversion
Reformers, crackers, oxidation reactors, chlorinators and polymerisation vessels. Catalyst fines, high pressure and exotherms define the mechanical demand.
Acid, Caustic & Brine Handling
Sulphuric, hydrochloric and phosphoric acid, caustic soda, hypochlorite and saturated brine — the shortest route to a failed pump in the whole plant.
Heat Exchange & Cooling
Shell-and-tube exchangers, air coolers and cooling towers. Fouling, scaling and tube-side erosion drive the shutdown schedule.
Separation & Filtration
Centrifuges, filter presses, decanters and crystallisers separate product from liquor. Filter feed lines run abrasive, high-solids and often hot.
Drying, Blending & Packing
Spray and rotary dryers, blending vessels and bagging lines finish the product. Dust, static and hygiene constraints govern here.
Utilities, Steam & Flare
Boilers, deaerators, cooling water, instrument air, nitrogen and the flare header. Utility failure trips the plant faster than any process fault.
Effluent & Emission Control
Neutralisation, oil separation, aeration, scrubbing and sludge handling — increasingly the section that decides whether the plant keeps its NOC.
What Actually Fails in a Chemical Plant
Ten problems every process and maintenance engineer in Pakistan recognises — and the engineering answer we apply.
Chloride Stress Corrosion Cracking
Plain SS304 and SS316 crack under tensile stress in warm chloride-bearing brine, cooling water or hypochlorite — often with no visible wall loss beforehand.
Sulphuric Acid Grooving
Concentrated acid protects steel with a film; velocity or dilution strips it and the line grooves through at bends and downstream of valves.
Hydrochloric Acid Attack
No common metal survives wet HCl. Metallic pumps and valves fail in weeks and leaks become a plant safety event, not a maintenance job.
Caustic Embrittlement in Hot Service
Hot concentrated NaOH cracks carbon steel around welds — the classic caustic evaporator and 50% caustic line failure.
Catalyst & Solids Erosion
Catalyst fines, crystals and filter cake wear vane tips, casing cutwaters and valve seats until head and shut-off are both gone.
Seal Failure on Hazardous Media
Single seals on solvent, acid or toxic service leak to atmosphere, forcing an unplanned isolation and an environmental report.
Valve Passing on Isolation
A gate or ball valve that will not shut off means the unit cannot be safely isolated, and the turnaround stalls before the first bolt is cracked.
Cavitation on Hot & Volatile Duty
Boiling-point liquids, condensate and light hydrocarbons flash in the suction; the impeller pits and the bearings fail within the run.
Obsolete Imported Equipment
Much of the installed base dates from the 1970s–1990s. Model numbers are discontinued, agents have closed and drawings were never handed over.
Turnaround Schedule Slip
Every day of an unplanned extension is lost production. Spares that arrive late, or arrive wrong, are the usual cause.
Equipment for Chemical & Petrochemical Duty
Manufactured, refurbished and reverse-engineered at our Lahore works. Drag the row or use the arrows.
Chemical Process Pumps
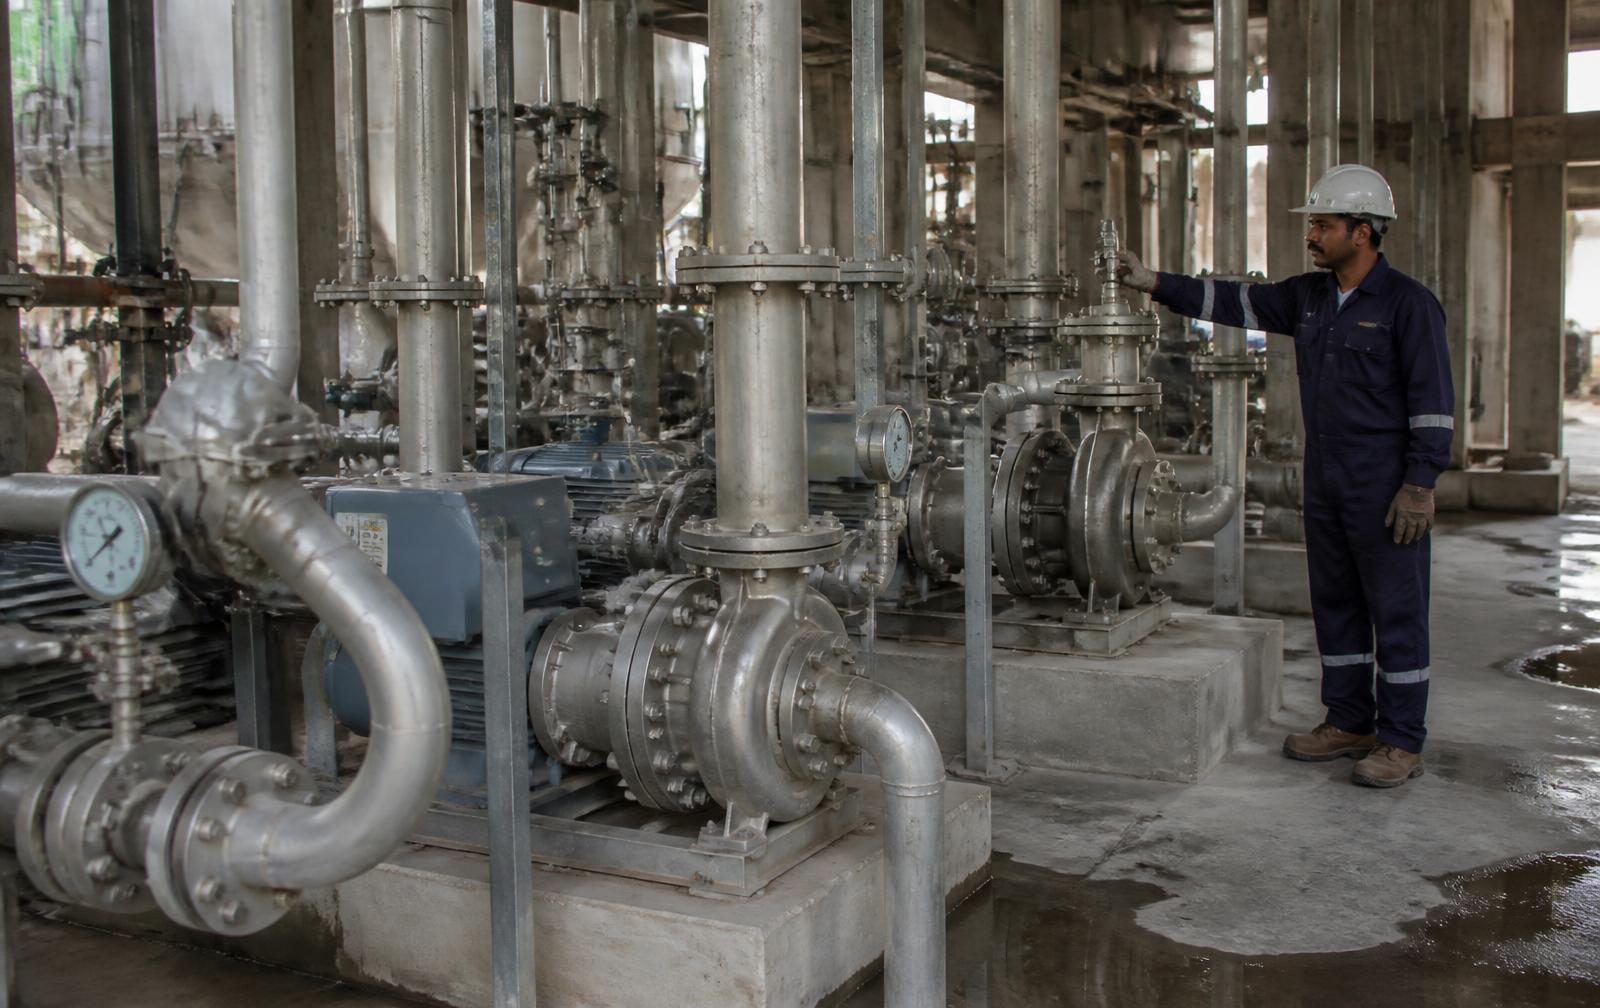
End-suction and back pull-out centrifugals to ISO 2858 / ISO 5199 envelope for solvents, liquors, condensate and general process transfer.
- 25–400 mm
- CF8M / CF3M
- to 500 m³/h
Acid & Caustic Pumps
Sulphuric, phosphoric, hydrochloric, caustic soda, hypochlorite and brine duty with metallurgy or lining selected against concentration and temperature.
- Alloy 20
- CD4MCu
- PTFE lined
Hot Oil & Hydrocarbon Pumps
Reflux, bottoms, transfer and hot oil sets with API 682 sealing, cooled bearing housings and centreline mounting for thermal growth.
- to 350 °C
- API 682 seals
- Centreline mount
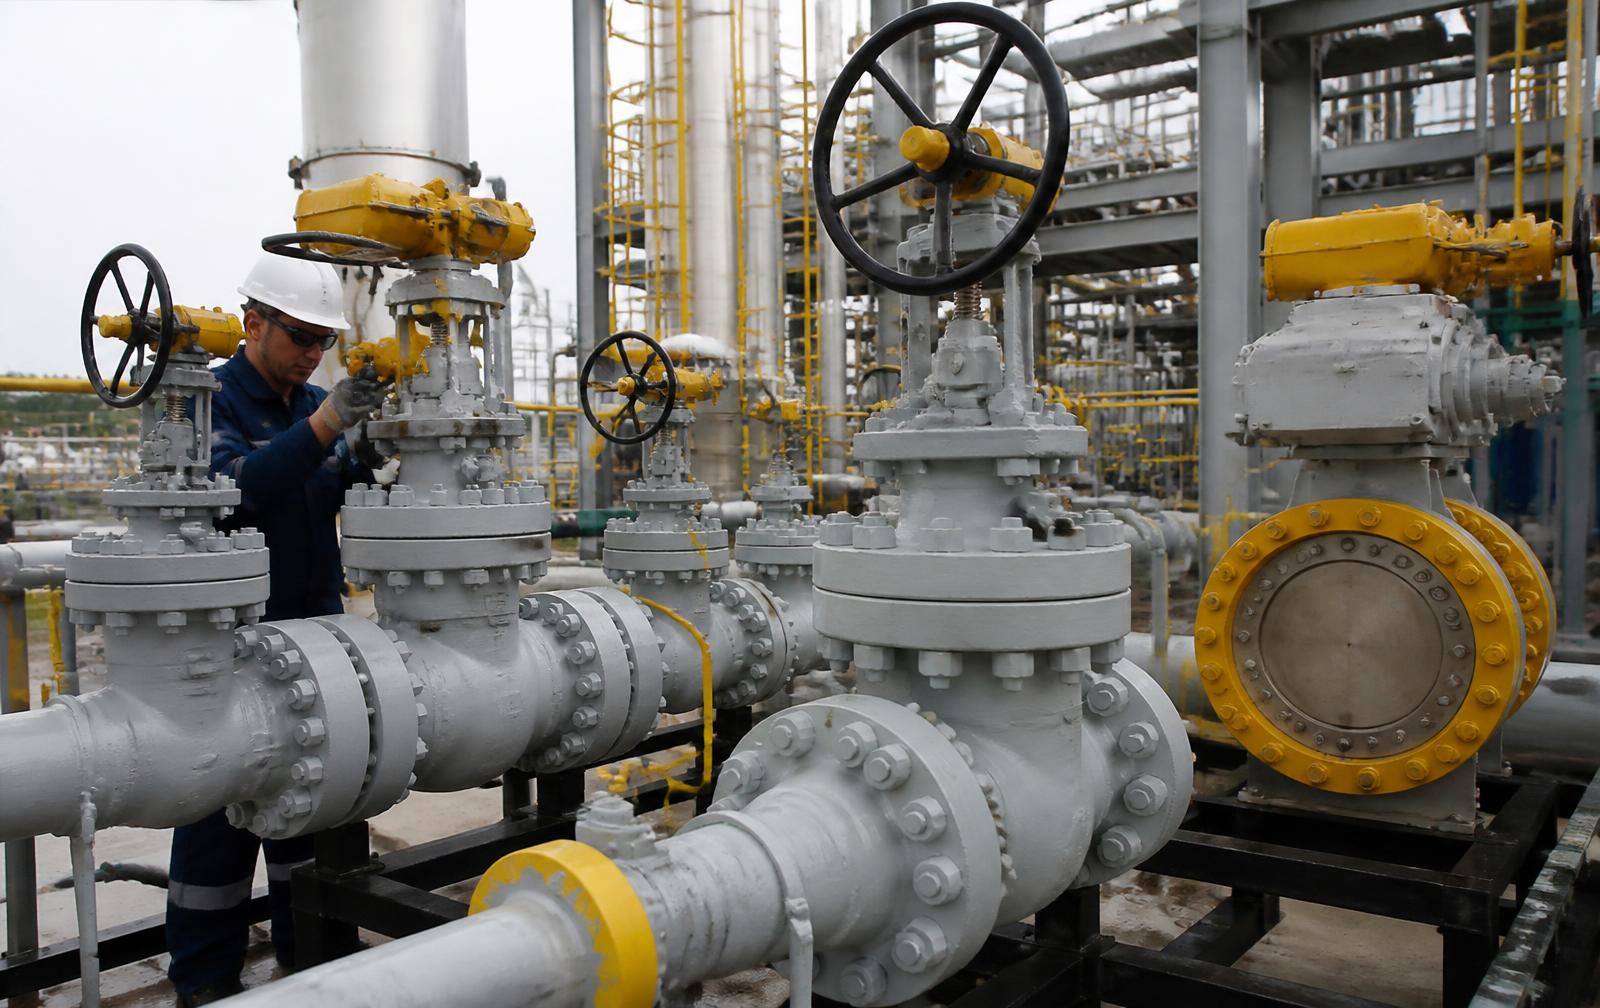
Gate, Globe & Non-Return Valves
Bolted-bonnet rising-stem gate, globe and swing or dual-plate check valves for process, utility and hydrocarbon isolation.
- 25–1200 mm
- PN10–PN40
- API 598 tested
Ball, Plug & Butterfly Valves
Floating and trunnion ball, sleeved plug and wafer or lugged butterfly valves with PTFE, RPTFE or metal seats, manual or actuated.
- to 2400 mm
- Fire-safe option
- Pneumatic / electric
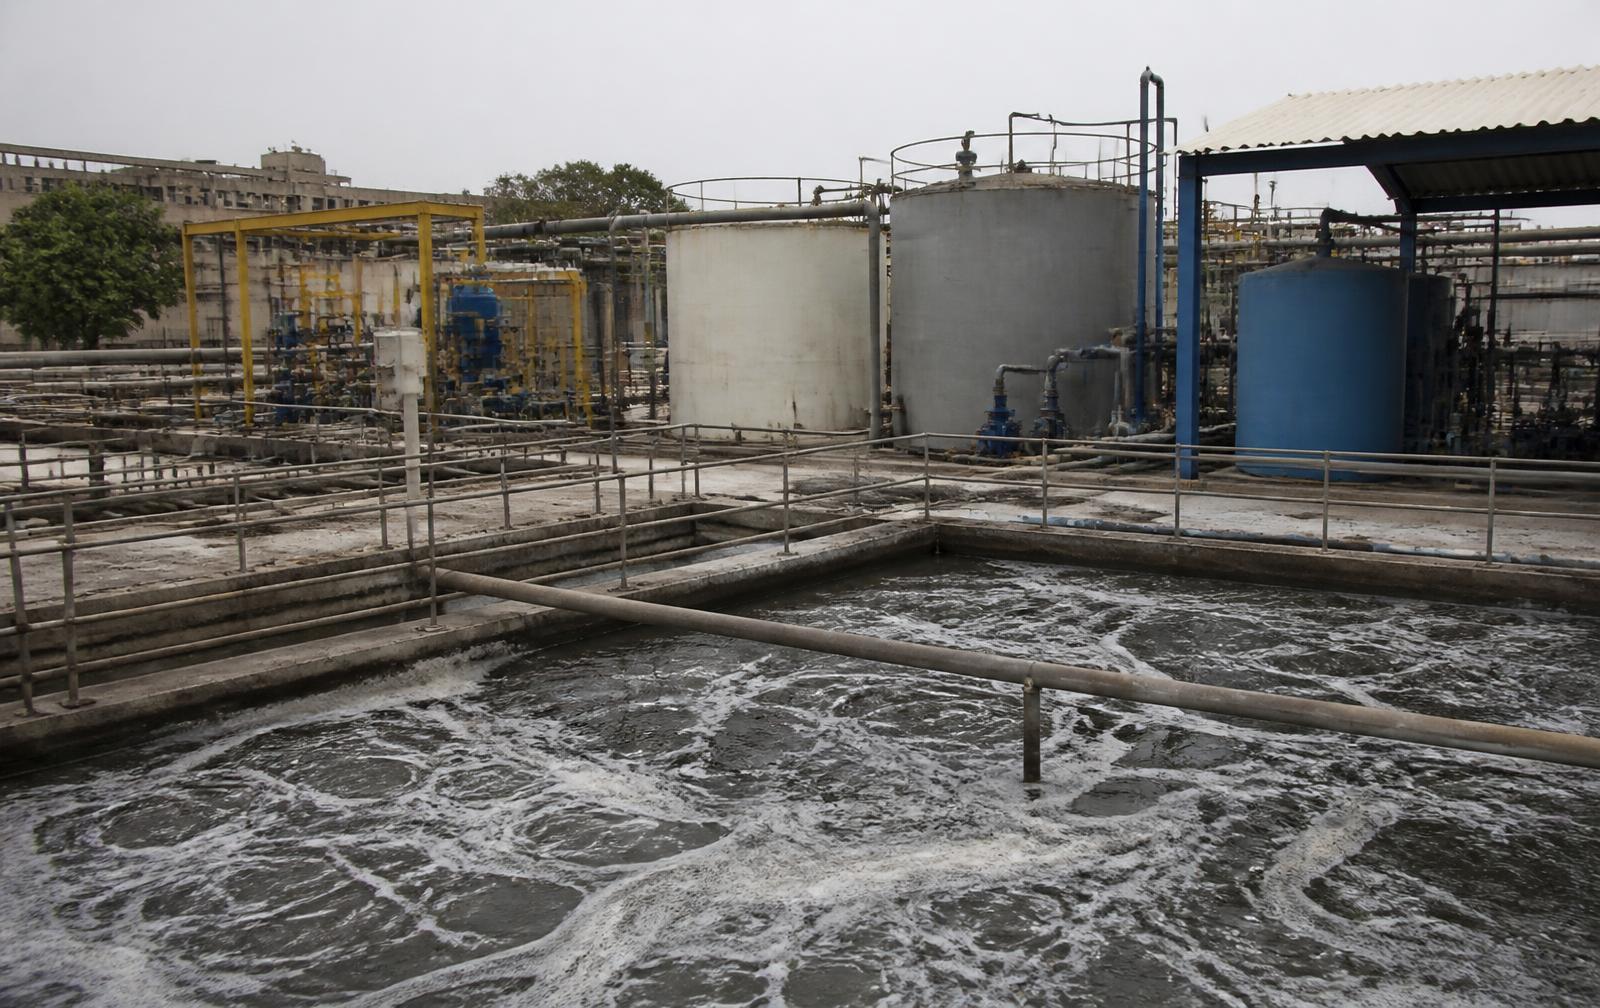
Slurry, Sludge & Dosing Pumps
Filter feed, catalyst slurry, gypsum, lime and sludge duty plus metering and dosing skids for neutralisation and scrubbing.
- 27% Cr
- Rubber lined
- Renewable liners
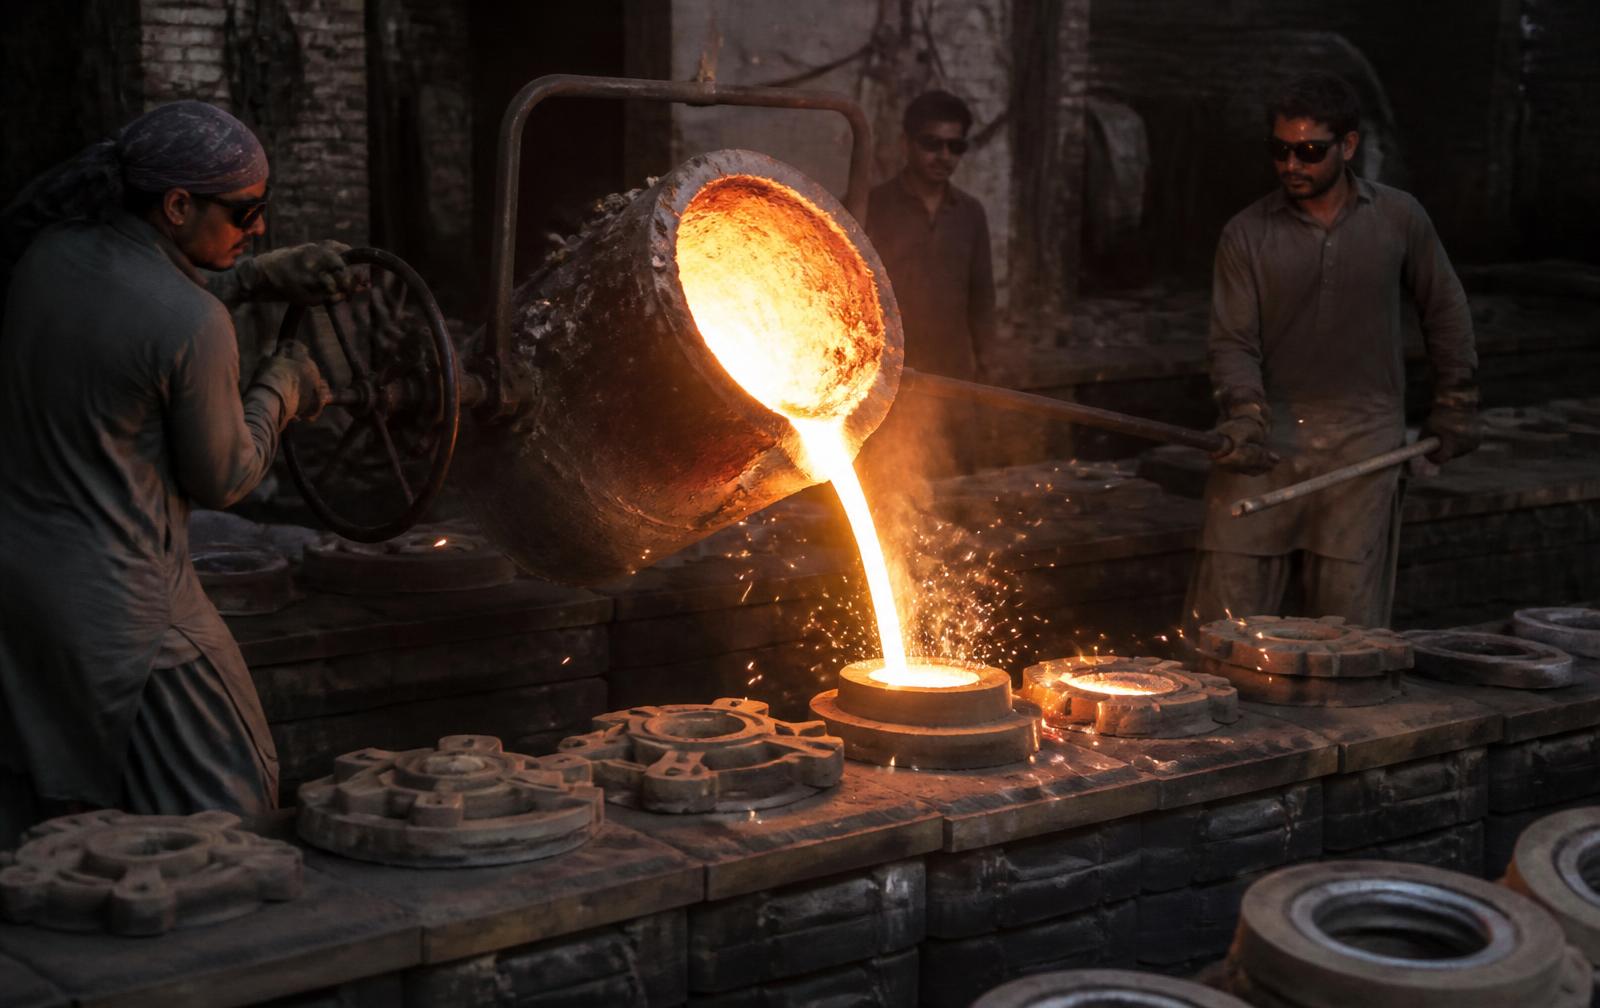
Alloy Castings & Reverse Engineering
Impellers, casings, discs, seats, bushes and housings in grey iron, ductile iron, bronze, CF8M, CD4MCu and Ni-Resist — from sample or drawing.
- Pattern making
- Spectro tested
- Any make
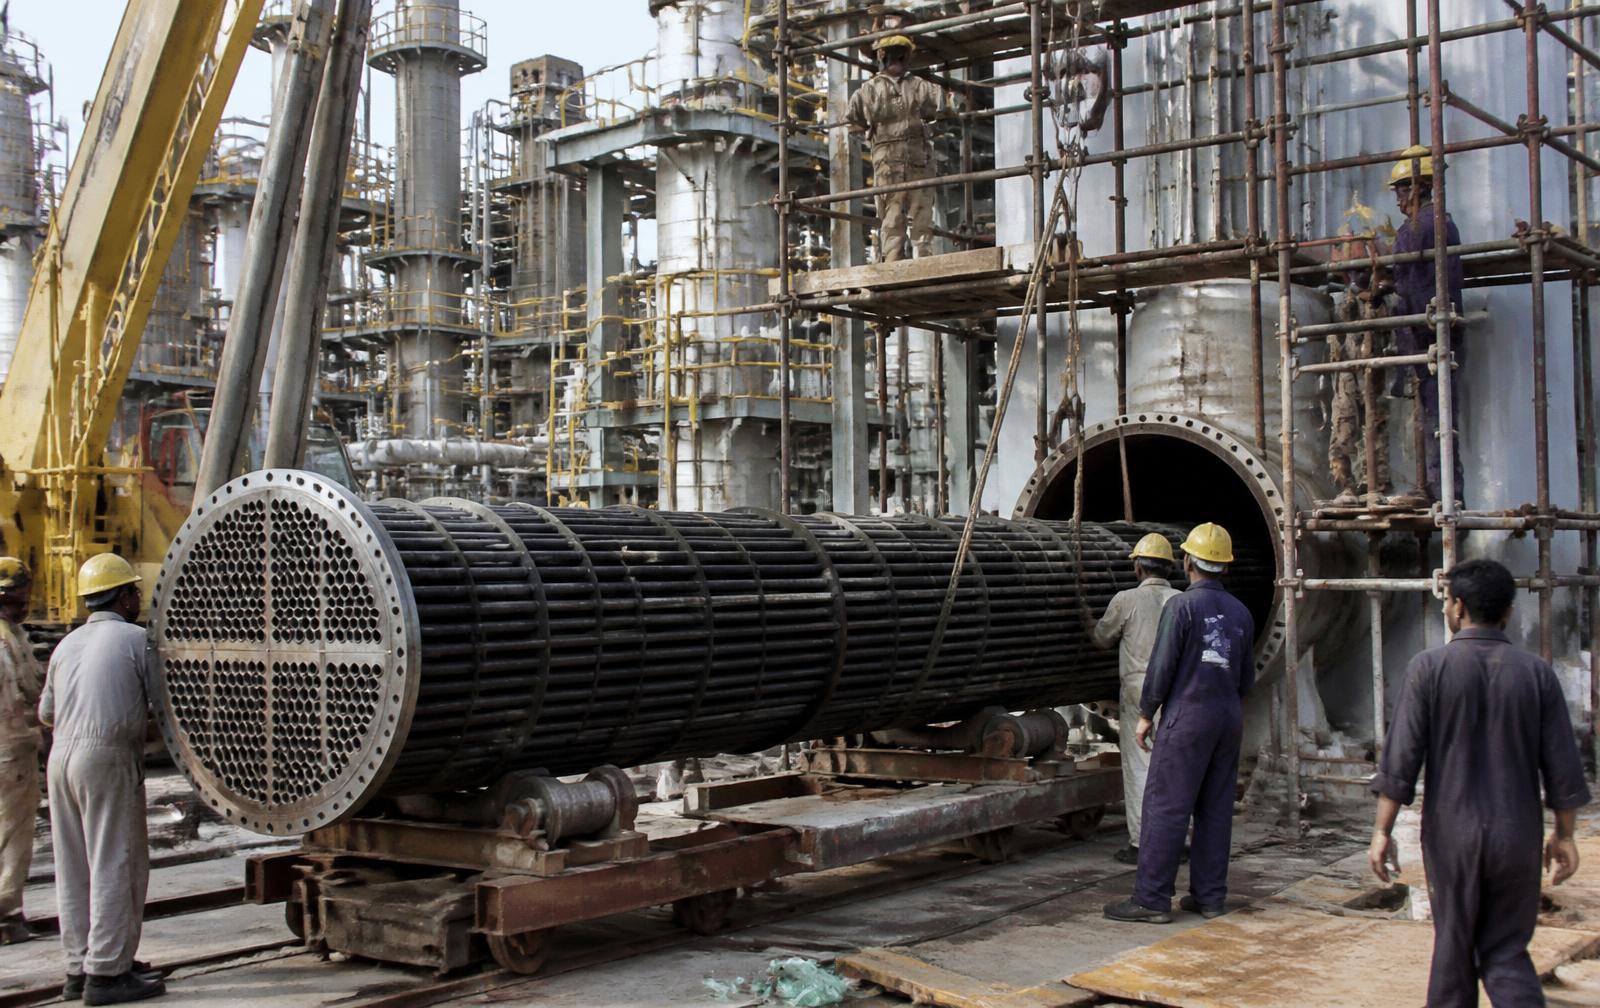
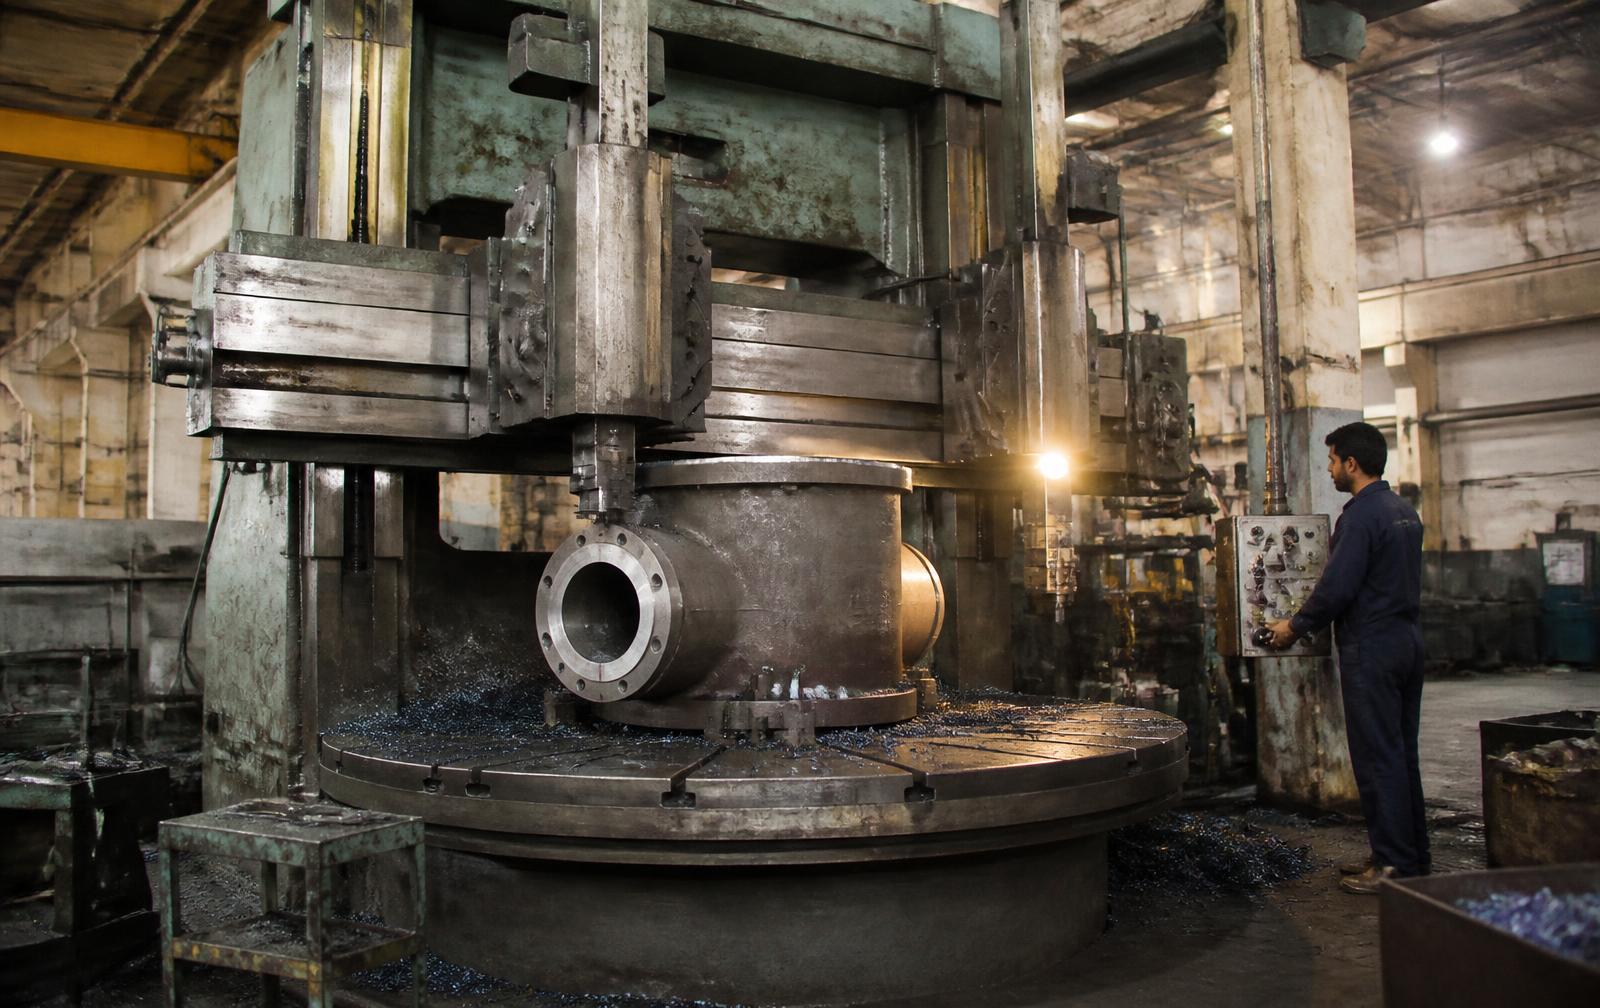
Exchanger & Vessel Machining
Tube plate drilling and refacing, channel cover and flange facing, nozzle repair and on-site turnaround support during shutdowns.
- Tube plates
- Flange facing
- Shutdown support
Where Each Product Is Installed
A schematic walk through a process plant. Hover a node or a line item to see the pairing.
Plants We Supply Across Pakistan
From Hub and Port Qasim to Faisalabad, Khewra, Hattar and Daharki — the equipment changes, the corrosion problem does not.
Chemical Plant Specification Sheet
Working figures our engineering office uses when sizing and selecting for Pakistani process plants.
| Service | Typical Flow | Head / Pressure | Temp | Key Consideration |
|---|---|---|---|---|
| General process transfer | 20–300 m³/h | 25–70 m | Ambient–120 °C | Chloride content drives grade selection |
| Hot oil / reflux | 50–400 m³/h | 40–140 m | 200–350 °C | Centreline mount; cooled bearings; API sealing |
| Sulphuric acid 93–98% | 5–80 m³/h | 15–50 m | 30–90 °C | Velocity limit ~1.2 m/s; Alloy 20 or Si-iron |
| Hydrochloric acid 30% | 5–60 m³/h | 15–40 m | Ambient–60 °C | Non-metallic or PTFE/PFA lined only |
| Caustic soda 32–50% | 10–120 m³/h | 20–60 m | 40–110 °C | Nickel alloys above caustic curve; PWHT |
| Saturated brine | 50–400 m³/h | 20–55 m | 40–70 °C | Chloride SCC; duplex preferred over 316 |
| Catalyst / filter slurry | 20–150 m³/h | 20–45 m | 50–140 °C | Abrasion; renewable liners; low tip speed |
| Boiler feed water | 30–250 m³/h | 40–120 bar | 105–150 °C | NPSH at saturation; rotor balance G2.5 |
| Cooling water | 200–3000 m³/h | 15–45 m | 32–45 °C | Fouling and biocide corrosion allowance |
| Effluent / sludge | 20–200 m³/h | 10–35 m | Ambient–60 °C | Rag and solids passage; non-clog impeller |
| Medium | Concentration / Temp | Recommended Material | Avoid |
|---|---|---|---|
| Sulphuric acid | 93–98%, <50 °C | Carbon steel (low velocity), Alloy 20, high-silicon iron | SS316 at high velocity |
| Sulphuric acid | <70%, any temp | Alloy 20, CD4MCu, PTFE lined | Carbon steel, cast iron |
| Hydrochloric acid | All strengths | PTFE / PFA lined, rubber lined, non-metallic | All common metals |
| Phosphoric acid | up to 54% P₂O₅ | CF3M, Alloy 20, duplex | Grey iron, bronze |
| Caustic soda | ≤50%, <65 °C | Carbon steel, CF8M, ductile iron | Bronze, aluminium |
| Caustic soda | ≥50%, >90 °C | Nickel 200 / nickel-clad, PWHT steel | As-welded carbon steel |
| Brine & hypochlorite | Saturated, 40–70 °C | CD4MCu duplex, titanium, lined | SS304 / SS316 |
| Hydrocarbons & solvents | up to 350 °C | Carbon steel, CF8M, 12% Cr trim | Elastomer-heavy designs |
| Abrasive slurry | Any | 27% Cr white iron, rubber lining, CA6NM | Soft stainless, bronze |
| Ammonia / carbamate | Urea synthesis | 316L urea grade, duplex 2205 / 2507 | Standard 316 |
| Valve Type | Size Range | Rating | Application |
|---|---|---|---|
| Gate (bolted bonnet, rising stem) | 25–1200 mm | PN10–PN40 / 150–300# | Process and utility isolation, tank farm |
| Globe & needle | 15–400 mm | PN16–PN40 | Throttling, steam, boiler house, sampling |
| Ball (floating / trunnion) | 15–600 mm | 150–300# | Hydrocarbon, solvent and gas isolation |
| Plug (sleeved / lined) | 25–300 mm | PN10–PN16 | Slurry, acid and abrasive liquor service |
| Butterfly (wafer / lugged / double flanged) | 50–2400 mm | PN10 / PN16 | Cooling water, brine, headers, large bore duty |
| Knife gate | 50–1200 mm | PN10 | Filter cake, gypsum, catalyst and sludge lines |
| Non-return (swing / dual plate) | 50–900 mm | PN16 / PN25 | Pump discharge protection, surge control |
| Diaphragm & pinch | 25–300 mm | PN10 | Dosing, corrosive and hygienic transfer |
| Lined (PTFE / PFA / rubber) | 25–600 mm | PN10 / PN16 | HCl, hypochlorite and aggressive acid lines |
| Sealing Option | Typical Plan | Best For | Notes |
|---|---|---|---|
| Gland packing (graphite) | Plan 32 flush | Water, non-hazardous liquor | Cheapest; leakage accepted and managed |
| Single cartridge seal | Plan 11 / 13 | Clean process liquids | Requires clean flush and vapour margin |
| Single with quench | Plan 62 | Crystallising and caustic media | Steam or water quench prevents seal-face build-up |
| Double / dual pressurised | Plan 53A / 53B | Toxic, flammable, acid duty | Barrier fluid at higher pressure; zero emission |
| Dual unpressurised | Plan 52 | Volatile hydrocarbons | Buffer fluid with vapour recovery |
| Magnetic drive / sealless | — | Hazardous or ultra-clean service | No dynamic seal; dry-run protection required |
| Area | Standard | Applied To |
|---|---|---|
| Quality system | ISO 9001:2015 | All manufacturing and inspection |
| Process pumps | ISO 2858 / ISO 5199 / API 610 where specified | Pump hydraulic and mechanical design |
| Pump testing | ISO 9906 Grade 2 | Performance run before dispatch |
| Shaft sealing | API 682 seal plans | Hazardous and hot service pumps |
| Valve testing | API 598 / BS EN 12266 | Shell and seat hydrostatic test |
| Fire-safe valves | API 607 / BS 6755 Part 2 | Hydrocarbon isolation, where specified |
| Butterfly valves | BS EN 593 / AWWA C504 | Water, brine and large-bore duty |
| Castings | ASTM A48 / A536 / A351 CF8M / A890 CD4MCu | Casings, impellers, discs, seats |
| Welding | ASME IX qualified procedures | Fabricated bodies, spools and lined pipework |
| Flanges & dimensions | ASME B16.5 / B16.34 / BS EN 1092 | End connections and pressure-temperature ratings |
| NDE | DP, MPI, UT, RT and PMI as specified | Castings, welds and incoming alloy verification |
Foundry, Machine Shop and Test Bay in Lahore
Pattern to painted, tested equipment under one roof — which is why a shutdown-critical spare can be turned around in days, not months.
Documented, Not Assumed
Every job leaves with a data pack: spectro and mechanical certificates, PMI where specified, dimensional report, NDE records, hydrotest and performance curves, and coating DFT sheets.
Pakistan's Chemical & Petrochemical Plants
From the Hub and Port Qasim complexes to acid, fertilizer and effluent plants upcountry.
Chosen by Process Engineers Since 1948
Metallurgy Matched to the Medium
Selection driven by concentration, temperature, chlorides and solids — with PMI and spectro evidence, not a vendor's word.
Any Make, Any Vintage
European, Japanese, American or Chinese plant. If a sample, drawing or measurement exists, we can manufacture the part.
Foundry to Test Bay
Casting, machining, assembly, painting and testing in one Lahore facility — no chain of sub-vendors to chase during a shutdown.
Turnaround Discipline
Pre-shutdown survey, agreed spares list, sequenced delivery and site presence for the critical path items.
Import Substitution in Rupees
Locally manufactured spares to the same or better specification — no LC, no six-month lead time, no foreign-currency exposure.
Documented Quality
ISO 9001:2015 system, material and NDE certificates, hydrotest records and witnessed testing on request.
Questions From Process & Maintenance Engineers
CF8M (SS316), CF3M, CD4MCu duplex, Alloy 20, Ni-Resist, high-silicon iron for concentrated sulphuric acid, PTFE and PFA lining for hydrochloric acid and hypochlorite, and rubber-lined wet ends for slurry and brine. Selection is made against concentration, temperature and chloride content — not against a catalogue page.
Yes. Most process plant in Pakistan is European, Japanese, American or Chinese supply. We reverse-engineer impellers, casings, shafts, sleeves, wear rings, valve discs, seats, gland assemblies and gearbox parts from a sample, an old drawing or a dimensional survey, with spectro analysis and material test certificates.
Yes. Gate, globe, ball, plug and non-return valves with bolted-bonnet construction, graphite packing, anti-static devices and fire-safe design references to API 607 / BS 6755 where the specification calls for it, hydrostatically tested to API 598 with certificates.
Bodies and casings are machined up to 2400 mm diameter on vertical turret lathes, with CNC turning, horizontal boring, gear cutting and dynamic balancing in the same works. Castings are poured in grey iron, ductile iron, bronze, stainless and duplex grades at our own foundry in Lahore.
Yes. Typical scope covers pre-shutdown survey and spares planning, removal, workshop overhaul of pumps and valves, exchanger and vessel machining, lapping and hydrotesting, re-installation, alignment, commissioning support and a written condition report with recommended spares for the next run.
By moving away from plain austenitic stainless where chlorides and temperature justify it — duplex CD4MCu or super duplex wetted parts, correct solution annealing, qualified welding procedures and PMI on incoming material before it enters the shop.
Every job leaves with a data pack: spectro and mechanical test certificates, dimensional report, NDE such as DP, MPI, UT or radiography where specified, hydrostatic shell and seat test records, ISO 9906 pump performance curves and coating DFT records.
Refineries and lube plants, chlor-alkali and PVC, PTA and polyester, soda ash, urea and ammonia fertilizer complexes, sulphuric and phosphoric acid plants, paints, resins and adhesives, pharmaceutical and agrochemical formulation, textile processing chemicals, tanneries, edible oil and industrial gas plants.
Yes. Single, double and cartridge mechanical seals to API 682 seal plans including Plan 11, 13, 32, 52, 53A, 53B and 62, plus magnetic-drive and sealless configurations where leakage of hazardous media is unacceptable.
Medium and concentration, temperature, specific gravity and viscosity, solids content, flow and head or differential pressure, line size and rating, existing make, model and tag number, area classification, and photographs or drawings of the part being replaced.
Send Us the Process Data
Tell us the medium and the deadline. Our engineering office replies with material selection, a technical proposal and a realistic delivery date — not a catalogue page.
- Unit and duty — tank farm, distillation, reaction, acid handling, utilities or effluent
- Medium, concentration, temperature, SG, viscosity and solids content
- Flow and head or differential pressure, line size and flange rating
- Existing make, model and tag number, with a photograph if available
- Whether this is a breakdown, a turnaround item or a new project
- Any client specification, area classification or standard to be met